Prepare the input
Tyre granulate is prepared for a uniform, consistent feed.
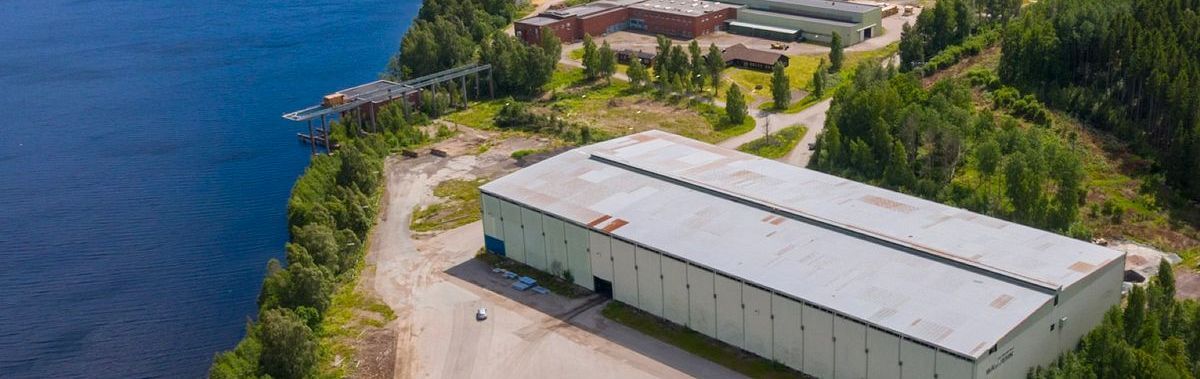
THE FACTORY / BILLINGSFORS, SWEDEN
A modular factory under development in Billingsfors, Bengtsfors Municipality. Designed to convert end-of-life tyres into useful materials through continuous industrial production.
PLANNED DESIGN CAPACITY
Design figures from RETYRA’s factory presentation. These describe the planned facility, rather than current production.
01 / THE MATERIAL JOURNEY
Tyre granulate is prepared for a uniform, consistent feed.
Continuous thermochemical conversion breaks down the material in an oxygen-free environment.
Oil, carbon and gas are separated into usable output streams.
Recovered syngas supplies process energy within the plant.
02 / INDUSTRIAL OUTPUTS
The design targets material recovery of at least 80% at full operation, with recovered gas reused for energy.
A recovered material for rubber and plastics.
A circular feedstock for refining and chemical industries.
Recovered gas reused inside the plant to supply process energy.
03 / DESIGNED FOR RELIABILITY
04 / PROJECTED RESOURCE IMPACT
The factory model aims to reduce tyre incineration, substitute fossil-based raw materials and reuse gas for process energy.
RETYRA project estimate from the supplied factory presentation. The presentation does not include the calculation methodology or independent verification; realised impact will depend on operating conditions and the comparison baseline.
05 / FROM BUILD TO OPERATION
Permits, procurement and preparation.
Construction and installation of process equipment.
Testing, commissioning and production ramp-up.
Move towards full industrial production.
Indicative build cycle from the factory presentation, measured from start of build. Phases overlap. This is not a confirmed Billingsfors construction schedule.